Skip to content
An Oem Fibc For Pharmaceutical Supplier designs and produces flexible intermediate bulk containers for controlled pharmaceutical-material handling. These containers may carry excipients, active ingredients, powders, or processing waste, depending on validated use. Unlike ordinary bulk bags, pharmaceutical-grade FIBCs require documented materials, controlled manufacturing, and traceable quality records. The supplier must understand filling, discharge, grounding, liner selection, and contamination-control risks. Small details matter. A poorly fitted liner can trap powder inside seams. Static buildup can also create serious process hazards.
Market evidence supports stronger attention to pharmaceutical packaging performance. Grand View Research identifies pharmaceutical packaging as a growing global sector, driven by stricter quality expectations and expanding drug production. Smithers’ pharmaceutical packaging forecasts also emphasize compliance, traceability, and improved material performance. These reports describe market direction, not automatic supplier qualification. That distinction is important. A growing market does not prove that every FIBC manufacturer is suitable.
A reliable OEM partner should provide material specifications, batch records, change-control procedures, cleaning controls, and relevant test certificates. Manufacturing should follow a documented quality system, with risk-based controls aligned with customer validation requirements. Depending on the application, buyers may request ISO 9001 certification, food-contact declarations, extractables data, or electrostatic-performance testing. Pharmaceutical use is never one-size-fits-all. A supplier should review powder characteristics, filling equipment, discharge design, and storage conditions before recommending a bag. Even experienced teams can overlook operator handling. Therefore, technical consultation, sample trials, and clear acceptance criteria remain essential when selecting an Oem Fibc For Pharmaceutical Supplier.
What Is an OEM FIBC Supplier for Pharmaceutical Use?
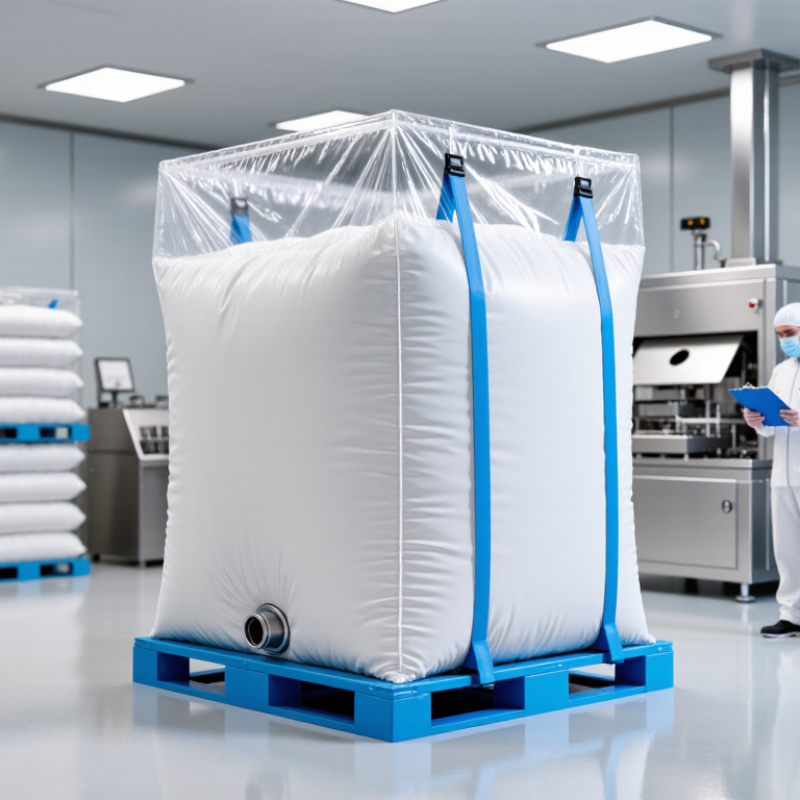
An OEM FIBC supplier designs and manufactures flexible intermediate bulk containers to a pharmaceutical company’s specifications. The supplier may customize bag dimensions, fabric strength, liner structure, filling ports, discharge outlets, and lifting loops. These containers support the controlled handling of powders, granules, and other approved pharmaceutical materials.
The supplier’s role extends beyond sewing fabric panels. It should provide documented material selection, controlled production, batch identification, and traceable inspection records. Pharmaceutical-grade FIBCs may require clean manufacturing areas, antistatic features, low-particle materials, and tested extractable limits. Each production lot should have defined sampling methods and release criteria. Small details matter. A loose thread or poorly sealed liner can affect handling and product protection.
An experienced OEM partner also supports design qualification and packaging validation. It can supply drawings, test reports, certificates, and change-control information for review by the customer’s quality team. However, the supplier does not replace that team’s final approval. Responsibilities must remain clear. In practice, specifications sometimes overlook warehouse stacking, discharge equipment, or operator access. That gap deserves attention. A technically strong design can still fail during routine use if the bag is difficult to lift, connect, or empty. Reliable cooperation includes trials, documented feedback, and careful correction when results are imperfect.
An OEM FIBC supplier for pharmaceutical use produces bulk bags to a customer’s specifications. The supplier may adjust dimensions, fabric strength, discharge openings, liners, and lifting loops. These changes must support safe handling and consistent production. Experience matters because small design errors can affect filling, transport, or discharge.
Pharmaceutical-grade OEM FIBC bags require carefully selected, low-shedding materials. Clean manufacturing areas help reduce dust and foreign particles. Conductive or antistatic fabric can control static risks during powder handling. Smooth inner liners may protect sensitive products from moisture and contamination. Every material should have documented specifications, inspection records, and suitable test results.
Traceability is essential. Each bag should connect to a production batch, raw material record, and inspection report. A reliable supplier can provide samples before full production. Customers should review seam strength, liner fit, load testing, and packaging conditions. Factory audits also reveal practical details that documents may miss.
No bag is perfect.
A thoughtful OEM process includes risk assessment and design review. The supplier should question unclear requirements instead of accepting every drawing blindly. Sometimes a requested feature creates cleaning or handling problems. That uncomfortable discussion can prevent costly failures. Quality systems, trained operators, controlled processes, and honest reporting build confidence over time. Even minor defects deserve investigation, because pharmaceutical packaging leaves little room for careless assumptions.
Key reference milestones for pharmaceutical-grade OEM FIBC bag design and control
Pharmaceutical-grade OEM FIBC suppliers typically align bag design, cleanliness control, electrostatic risk management, documentation, and qualification with applicable industry standards. ISO 21898:2004 covers flexible intermediate bulk containers, IEC 61340-5-1:2016 provides electrostatic-control guidance, and EU GMP Annex 1:2022 is relevant when FIBCs support sterile pharmaceutical processing. These references support supplier evaluation but do not replace product-specific validation, testing, or customer qualification.
An OEM FIBC supplier for pharmaceutical use manufactures flexible intermediate bulk containers to a buyer’s exact material, design, and documentation requirements. The package may hold powders, granules, or excipients, but it is not automatically suitable for pharmaceutical contact. Qualification must begin with a documented risk assessment.
Manufacturing should follow GMP principles, with controlled raw materials, approved suppliers, validated cleaning, and batch-level traceability. ISO 21898:2004 provides test guidance for FIBCs, including construction, lifting safety, and performance. For pharmaceutical applications, buyers should also review liner compatibility, seal integrity, particulate control, extractables, and leachables. USP General Chapter <661.1> offers a useful framework for evaluating plastic packaging materials. Small details matter. A loose thread can become contamination.
Quality control should include incoming-material inspection, dimensional checks, fabric strength testing, liner leak testing, visual examination, and a certificate of analysis for every lot. Where the product risk requires it, bioburden and endotoxin testing should be defined by written specifications. The FDA Drug Shortages Task Force report estimated that about 80% of active pharmaceutical ingredients used in the United States came from overseas sources. That dependence makes supplier audits and change notification essential. A qualified OEM should preserve samples, control artwork and specifications, and investigate deviations through documented CAPA procedures. No checklist is perfect. In practice, cleaning records may look complete while process weaknesses remain unnoticed. Regular audits, operator training, and honest deviation reporting are therefore more valuable than polished paperwork alone.
An OEM FIBC supplier for pharmaceutical use designs and manufactures flexible intermediate bulk containers to a customer’s technical requirements. The process begins with the product, not the bag. Powder density, flow behavior, moisture sensitivity, filling method, and discharge equipment all influence the specification.
Customization may include food- or pharmaceutical-grade fabrics, low-lint construction, conductive or antistatic options, and fitted polyethylene liners. The supplier should define fabric weight, seam design, safe working load, and lifting-loop configuration before production. Clean manufacturing areas, controlled handling, and documented inspection help reduce particulate and contamination risks. Small details matter.
The supply process normally includes technical review, drawing approval, material selection, prototype production, and performance testing. Testing may cover dimensions, load strength, grounding continuity, liner integrity, and powder flow during discharge. Each production batch should have clear identification and traceability records. Certificates of analysis and inspection reports should match the agreed specification.
A reliable OEM partner also uses change-control procedures. Any change to fabric, liner material, sewing method, or production location deserves documented review. Samples should be evaluated in the customer’s actual filling and unloading system. Laboratory results cannot predict every handling problem. Sometimes, a container performs well during testing but needs a revised spout or liner in routine operation. That feedback should improve the next design rather than disappear in paperwork.
| Data Dimension | Typical Pharmaceutical FIBC Requirement | OEM Customization Options | Supply and Quality Considerations |
|---|---|---|---|
| Supplier Role | An OEM FIBC supplier manufactures flexible intermediate bulk containers to a pharmaceutical customer’s approved design, specifications, and quality requirements. | Product design, construction, labeling, documentation, packaging, and delivery configuration can be adapted to the customer’s process. | The supplier should be able to provide controlled production records, traceability, change notification, and agreed inspection documentation. |
| Primary Application | Handling and transport of powders, granules, crystals, excipients, active pharmaceutical ingredients, and other dry bulk materials. | The bag may be configured for filling, discharge, lifting, storage, containment, or integration with pharmaceutical processing equipment. | The final design must match the material’s flow behavior, bulk density, sensitivity to moisture, electrostatic properties, and containment needs. |
| Fabric Material | Woven polypropylene is commonly used because it provides a high strength-to-weight ratio and can be converted into lifting and containment components. | Coated or uncoated fabric, conductive or dissipative yarns, liner compatibility, fabric weight, and seam construction may be specified. | Material specifications should identify polymer type, fabric construction, coating details, and applicable certificates or test reports. |
| Cleanliness Level | Pharmaceutical-use FIBCs generally require controlled cleanliness, low visible contamination, and protection against foreign-particle introduction. | Options may include controlled assembly, dedicated production areas, filtered air handling, protective inner packaging, and validated cleaning procedures. | Cleanliness claims should be supported by documented procedures, inspection criteria, sampling plans, and batch records rather than by appearance alone. |
| Liner Selection | A liner can improve product contact protection, reduce powder leakage, and help control moisture or cross-contamination risks. | Film type, thickness, shape, fit, opening, discharge port, closure method, and liner attachment can be customized. | The liner material should be evaluated for compatibility, extractables and leachables requirements, seal integrity, and intended storage conditions. |
| Electrostatic Control | Type A, B, C, or D FIBC constructions may be selected according to the powder’s ignition sensitivity, facility grounding system, and operating environment. | Conductive threads, grounding tabs, dissipative components, antistatic liners, and marking arrangements can be incorporated into the design. | Electrostatic performance must be assessed using an applicable test method and verified with documented inspection and grounding procedures. |
| Safe Working Load | Common rated capacities are approximately 500–2,000 kg, but the correct rating depends on the design, filling density, lifting method, and handling cycle. | Panel dimensions, loop configuration, lifting arrangement, safety factor, discharge system, and reusable or single-trip construction may be specified. | The safe working load must be supported by design calculations, seam-strength testing, lifting tests, and clear handling instructions. |
| Filling and Discharge | Top filling and bottom discharge are widely used for dry pharmaceutical materials, with closure systems selected to limit leakage and exposure. | Top spout, duffle top, conical top, flat bottom, discharge spout, iris closure, flap, or full-open bottom designs may be selected. | The outlet design should be checked against powder flowability, required discharge rate, operator ergonomics, and cleaning or disposal procedures. |
| Traceability | Each production lot should be identifiable through a batch or lot number linked to raw materials, operators, equipment, inspections, and release status. | Labels, barcodes, QR codes, customer part numbers, production dates, and serialized identification can be added where appropriate. | Traceability records should be retained according to the quality agreement and applicable customer or regulatory requirements. |
| Testing and Inspection | Typical controls include dimensional inspection, fabric and seam checks, visual cleanliness inspection, liner checks, and load-related testing. | Inspection frequency, acceptance limits, sampling level, test methods, and release criteria can be defined in the technical specification. | A documented quality plan should distinguish between in-process controls, final inspection, and customer-specific qualification testing. |
| Documentation Package | A package may include a certificate of conformity, lot information, material declarations, inspection results, and packaging or shipping records. | Additional documents may include drawings, specifications, change-control records, test reports, cleaning statements, and questionnaires. | Document requirements should be agreed before production and aligned with the customer’s supplier-qualification and quality-system procedures. |
| OEM Development Process | The process normally moves from application review to design approval, prototype or sample evaluation, testing, qualification, and routine production. | The customer can approve drawings, samples, artwork, packaging instructions, inspection plans, and production reference standards. | Formal approval gates help prevent unauthorized changes to dimensions, materials, seams, liners, labeling, or manufacturing locations. |
| Standards and Compliance | Requirements may involve packaging GMP principles, material-contact assessments, transport regulations, electrostatic standards, and customer-specific procedures. | The supplier can prepare compliance statements and test documentation based on the intended market, product, and handling environment. | No single standard covers every pharmaceutical FIBC application; compliance must be assessed against the actual use case and destination market. |
| Production Lead Time | A standard production order may require several weeks, while a new customized design generally requires additional time for engineering, sampling, testing, and approval. | Lead time is affected by design complexity, special fabric or liner materials, testing requirements, order quantity, and packaging specifications. | The purchasing schedule should separate sample approval, raw-material procurement, production, quality release, and transportation time. |
| Supplier Selection Criteria | A suitable supplier should demonstrate consistent manufacturing capability for clean, traceable, and application-specific bulk packaging. | Evaluation may cover customization capability, technical support, sample development, packaging options, and response to engineering changes. | Key checks include quality-system maturity, audit readiness, testing capability, supply continuity, complaint handling, and documented change control. |
An OEM FIBC supplier for pharmaceutical use designs bulk bags to a buyer’s specifications. These specifications may include liner material, filling ports, discharge systems, static-control features, and cleanroom packaging. The bag is not merely a container. It can affect contamination control, material flow, and operator safety.
Supplier evaluation should begin with documented GMP practices and traceability. Request resin certificates, batch records, inspection reports, and change-control procedures. ISO 21898 covers flexible intermediate bulk containers, but certification alone does not prove pharmaceutical suitability. Review cleaning validation, microbial controls, and extractables data for product-contact components. Ask to inspect the sewing area. Dust on floors, exposed fibers, or unclear personnel controls deserve attention. Small details matter.
Performance evidence should be practical. Require drop testing, safe working load data, electrostatic assessments, and liner integrity tests. Compare these results with the intended powder density and filling method. IQVIA’s Global Use of Medicines 2024 projects worldwide medicine spending to reach about 2.3 trillion dollars by 2028, increasing pressure on scalable and dependable packaging systems. Supplier capacity should therefore include backup production, controlled subcontracting, and realistic lead-time records. Audit responses should show CAPA effectiveness, not polished promises. No checklist is perfect. A pilot batch may still reveal awkward discharge, weak labels, or difficult handling. Evaluate the supplier through samples, site evidence, transparent data, and repeated communication before approving the OEM relationship.